¶ What gases and regulators do I need?
There is no one bottle that does fiber cutting, CO₂, welding and cleaning. Tell the gas shop the gas, purity, max inlet, working pressure and flow for your serial number. Then read this with the owner FAQ on the two rear ports — that is the bit people get wrong and then buy a new cutting head.
¶ Process map
| Process | Common gas role | What must be verified |
|---|---|---|
| Fiber cutting carbon steel | Oxygen may support exothermic cutting | Material/process table, purity, pressure/flow, oxygen-compatible system |
| Fiber cutting stainless/aluminum | Nitrogen or clean dry compressed air may eject melt | Required flow, pressure, purity/dew point/oil carryover, edge expectations |
| CO₂ cutting/engraving | Air or process-specific assist | CO₂ head/process documentation and material safety |
| Handheld welding | Shielding gas protects the molten weld | Alloy/joint procedure, gas type/purity/flow and draft control |
| Handheld cutting | Assist gas clears the kerf | Head/nozzle/process table and rated supply |
| Cleaning | Gas/air may protect optics or clear plume in a documented setup | Exact head instructions; extraction still required |
This table is the job, not a setpoint. A number from a manual screenshot or a forum post belongs to that head, that regulator, that alloy — not automatically to yours.
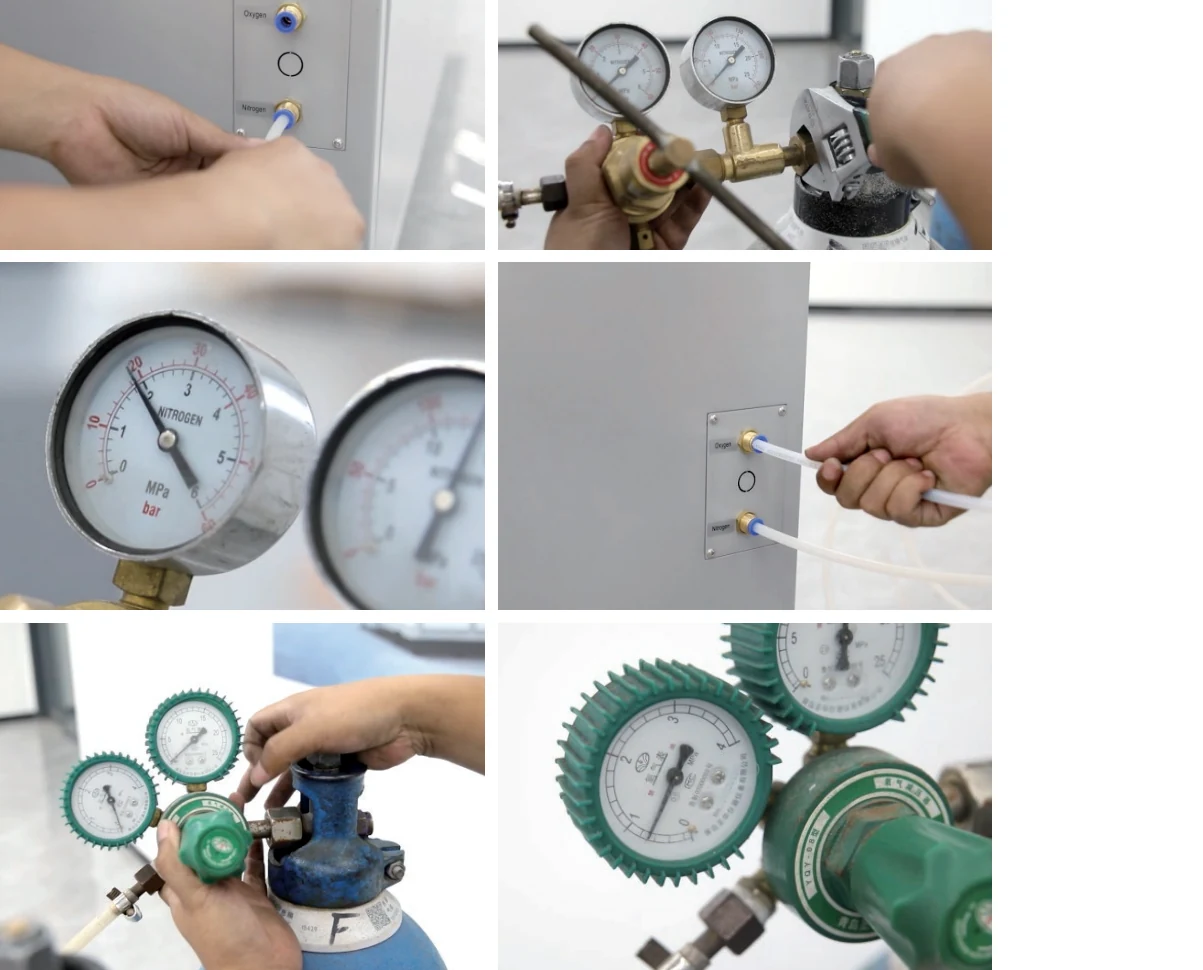
¶ Regulator and plumbing checklist
- Regulator is made for the specific gas and cylinder valve standard.
- Every regulator, hose, fitting, valve, filter, and machine inlet is rated for the maximum possible upstream pressure and required flow.
- High-flow service is sized by flow under pressure, not only the gauge's maximum number.
- Oxygen components are oxygen-compatible and kept completely free of oil/grease/contamination.
- Compressed air intended for a cutting process meets the required cleanliness, dryness, and oil limits.
- Cylinders are upright, secured, protected from impact/heat, and moved with caps/trolleys under local rules.
- Connections are leak-tested using an approved method—never a flame.
- The operator can isolate gas quickly and read both supply and downstream pressure.
¶ Why pressure alone misleads
The gauge can look fine while a small regulator, frozen regulator, clogged filter, long skinny hose, closing solenoid, or almost-empty bottle cannot keep flow during a pierce. Watch what happens while the nozzle is flowing. Then decide if the problem is supply, regulator, plumbing, or the machine.
¶ Owner-community values
Owners talked through dry air, high-flow regulators, and purity on the community gas thread. Those numbers are peer notes. Check them against your serial’s docs and a gas shop that actually understands laser cutting.
¶ Stop conditions
Close/isolate the supply for a damaged regulator/hose, uncontrolled leak, regulator icing with unstable delivery, contamination of oxygen hardware, incompatible fitting, unexplained pressure loss, or gas entering an area without adequate ventilation. Never alter relief devices or make fittings “fit” with adapters not rated for the service.
¶ Official Gweike video
These are Gweike's own walkthroughs. Keep the checks above, watch the sequence, then prove the result on your machine.