¶ Set up the wire feeder and weld
Get the joint fit, cleanliness, wire, gas, tip, and work-clamp connection right before touching power. More power will not close a bad gap, clean the joint, or fix wire that will not feed.
¶ Before enabling the source
- Establish the controlled laser area, barriers, correct PPE, extraction, fire watch, and emergency response.
- Identify base alloy, thickness, coating, oil, and filler requirements; remove contamination using a safe method.
- Confirm the handheld welding head, correct tip/nozzle, intact protective optics, and matching software mode.
- Secure shielding-gas equipment, use compatible rated regulator/hoses, and leak-test.
- Attach the work/ground clamp to clean conductive material in the documented arrangement.
- Route the head bundle and wire-feed lead clear of heat, sharp edges, and feet.
Welding fumes can contain hazardous metal compounds. Use local exhaust positioned to capture the plume without pulling shielding gas away from the weld; see NIOSH's welding guidance.
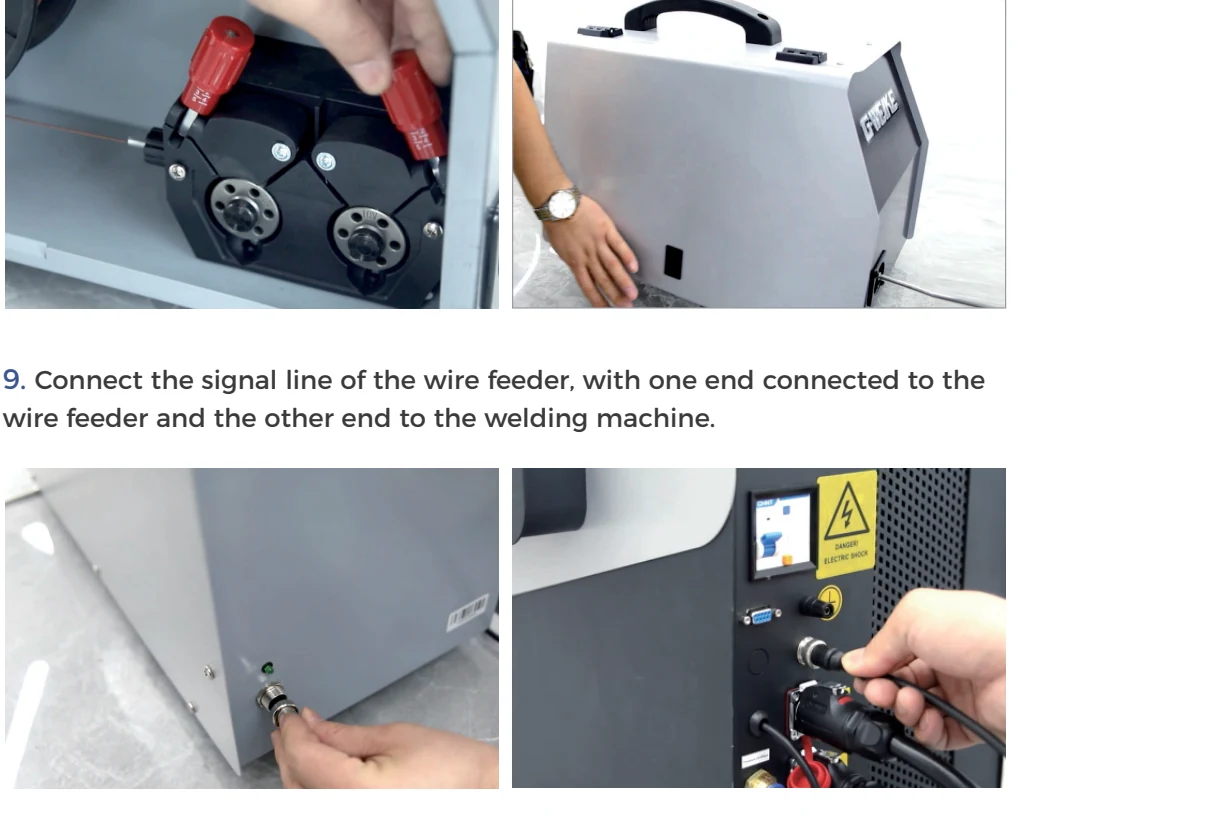
¶ Set up the wire feeder
- Choose filler wire compatible with the base material and process plan.
- Fit the correct drive roll/groove, liner, contact path, and guide for wire diameter.
- Load the spool in the intended feed direction and secure it without excessive drag.
- Thread wire with laser output disabled and hands clear of the drive mechanism.
- Set just enough roll pressure to feed reliably without crushing/deforming wire.
- Test inch/jog into a safe container; verify smooth feed and consistent exit position relative to the weld point.
¶ Make the first coupon weld
Use representative scrap prepared like the real joint. Start from the Gweike-supplied baseline for source power, material, thickness, joint, scan width/pattern, speed, gas, and wire. Confirm the head/workpiece geometry specified for the process; brace yourself and the work so the head cannot sweep toward a person or reflective path.
Enable the system only when the area is secured. Establish gas as required, position the head, engage safety/contact conditions, then trigger and move smoothly along a short coupon. Release the trigger before moving away; maintain post-flow if configured. Treat the part as hot.
¶ If the weld is unstable
| Symptom | Check before adding power |
|---|---|
| Intermittent start | Work clamp/contact safety, trigger/control connector, software ready state |
| Porosity/oxidation | Cleanliness, gas identity/flow/stability, drafts, nozzle position |
| Wire stubs or wanders | Wire path, roll pressure, feed speed, tip alignment, travel consistency |
| Excess spatter/undercut | Joint fit, focus/stand-off, scan width, speed/energy balance |
| Shallow fusion | Material/joint, travel speed, focus, process baseline, actual source output |
| Quality degrades over time | Protective window/tip contamination, gas decay, heat buildup, cooling alarm |
Stop for any protective-window damage, unstable optical connector, unexpected emission, persistent source alarm, fire, or a safety circuit that can be triggered incorrectly. Cut and inspect coupons when procedure qualification matters; surface appearance alone does not prove penetration or structural performance.
¶ Official Gweike walkthroughs
These are Gweike's own walkthroughs. Keep the checks above, watch the relevant sequence, then prove the weld on your machine.
12. Welding materials of different thicknesses
Weld coupons of different thickness using the on-source material/thickness row, not a guessed power number.
13. Handheld welding
Handheld weld: wire feeder, liner, spool, matched tip, documented focus offset, ~0.2 MPa class shielding as a starting check, ground on bare metal, then enable feed, emission, and red light on scrap.
26. Welding-gun optical coaxial adjustment
Weld-gun coaxial / red-beam to wire alignment. A wire that is not on the spot welds beside the joint.
For table-mounted rather than handheld welding, use the separate CNC-table welding and cleaning guide. Open the complete official playlist.