¶ Rotary cleaning, welding, and quenching
You have an open laser beam and a powered rotating shaft in the same job. Set up the rotary, head, work clamp, gas, extraction, and programmed motion as one guarded system. This is not a handheld job with a motor added beside it.
Danger: Two independent hazards
Prevent access to the beam/reflection zone and to entanglement points. Do not hand-hold the head against a powered rotating shaft unless the exact engineered Gweike setup and risk assessment explicitly provide for it. Secure the head/fixture as documented, contain reflections, and keep bundles from winding around the work.
¶ Assess the job
Identify substrate, coating/contamination, diameter, length, mass, runout, process objective, and required qualification. “Quenching” or surface hardening changes metallurgy; validate hardness profile, cracking, distortion, and application requirements with competent process engineering rather than appearance alone.
For cleaning, identify the removed material and its waste/filter requirements. For welding, identify base/filler material, joint, shielding gas, and inspection standard. Provide local extraction without disrupting shielding or entering the beam path.
¶ Configure under isolation
- Save the flat-bed and existing handheld configurations.
- Secure and support the shaft; rotate by hand through a full revolution.
- Install the rotary and the process head/fixture following their exact documented connections.
- Route optical/control/gas/wire-feed/extraction services so neither rotation nor travel can catch them.
- Select the matching cleaning, welding, or supported treatment mode and a verified baseline.
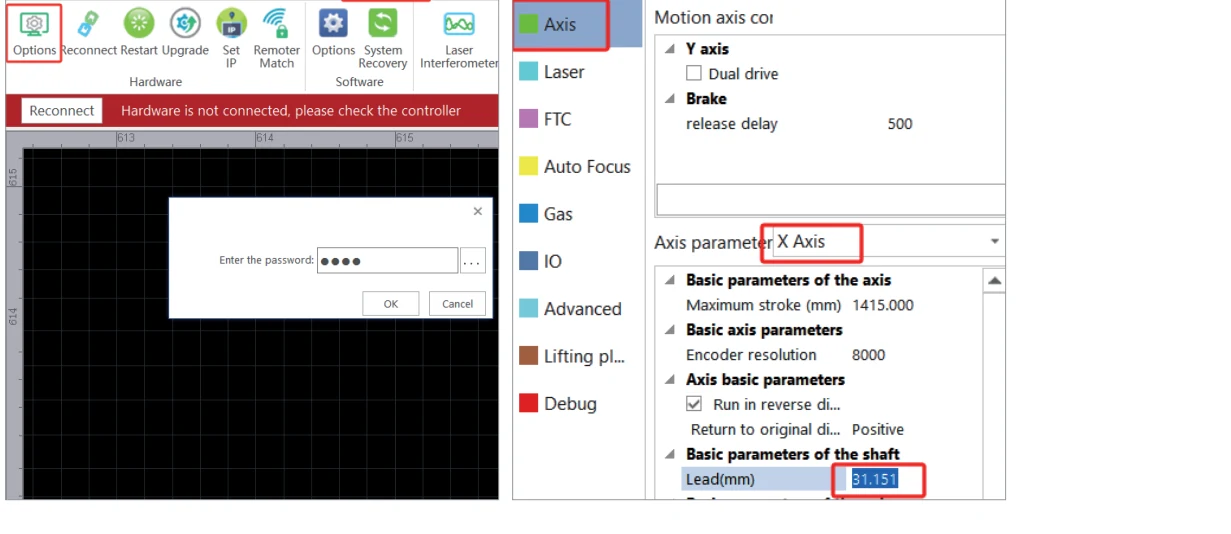
- Configure rotary direction and lead/ratio from measured geometry.
¶ No-emission proof
With output disabled, run the planned rotation and any linear travel at reduced speed. Check start/end location, overlap/pitch, head clearance, chuck/support clearance, direction, emergency stop, and cable behavior through the complete cycle. Mark a reference line on the shaft to detect slip.
¶ Process a test band
Use a short low-consequence band with the same preparation as the real part. Start extraction/gas, secure the controlled area, and supervise. Evaluate uniformity around the full circumference, seam overlap/gap, heat, substrate condition, weld penetration or cleaned residue as relevant.
Stop for shaft slip/whip, bundle movement, unstable ready/trigger state, unexpected beam path, uncontrolled plume/fire, metallurgical damage, head/optic contamination, or any source/cooling/motion alarm.
After processing, isolate the system before inspection and follow calculate lead and restore axes.