¶ CNC-table welding and cleaning
This is welding and cleaning on the CNC table, not with the handheld gun. Different optical path, different FTC. If the floating head was just cutting, do the official “shield the FTC” prep before you run a table-weld program.
¶ Shield the FTC before CNC weld/clean
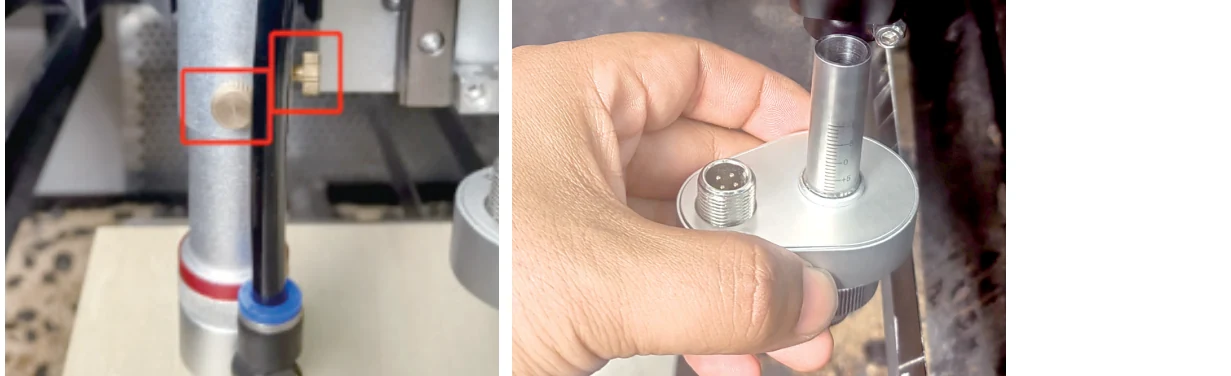
The official clip is preparation. The height controller used for cutting can false-trigger or crash when you are no longer doing capacitive cutting. The factory sequence disables/shields that FTC path as documented for this mode, then restores it before the next cutting job. This is not “jumper the alarm and keep cutting.” If you cannot restore cutting height control afterwards, stop.
¶ CNC laser welding
The official table-weld video walks fixture, ground, gas, and a parameter row for a plate joint. Check these before you copy the video:
- Ground is on the workpiece, not on a painted fixture.
- Shielding gas is the one in the weld row, at a flow that is not blown away by shop draft.
- Travel is programmed; this is not handheld weaving.
- Stay off oxygen-cut residue and mill scale if the row assumes clean metal.
¶ CNC laser cleaning
The official table-clean video is a programmed raster/path, not a handheld sweep. Cleaning still produces fume and can throw debris at the window. Run extraction. Do not aim a clean path at a reflective pocket that sends energy back into the head. After the job, restore the cutting head, FTC, and a known-good cutting XML before the next cut.
Related: change to handheld, handheld welding, handheld cleaning.